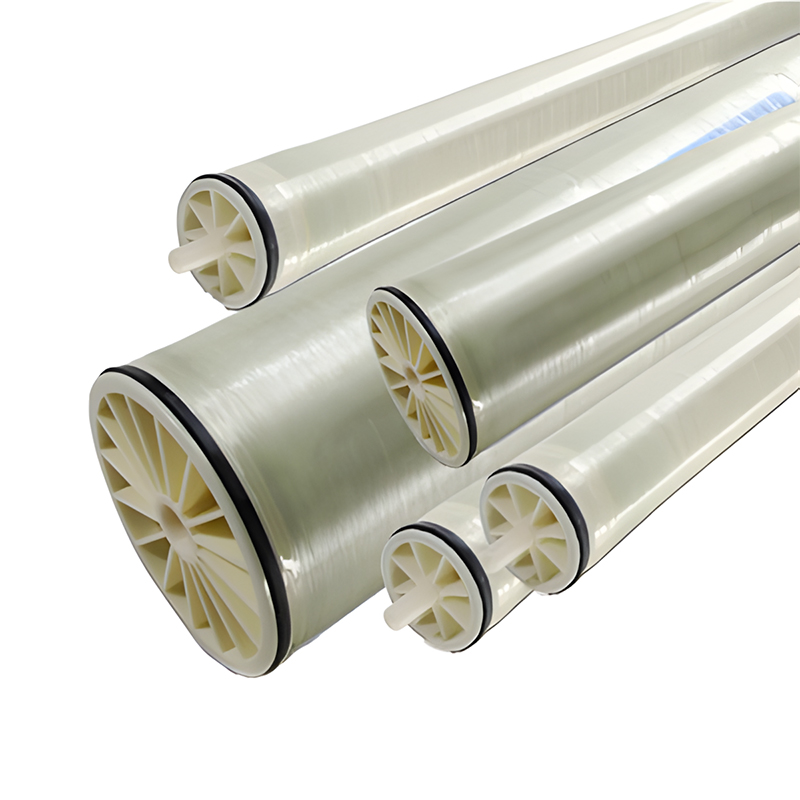
This technical guide provides a standards-aligned interpretation of diffusion dialysis acid recovery membranes developed by Shanghai Smax New Materials Technology Co., Ltd. As a supplier with over 10 years of R&D and industrial experience in homogeneous ion exchange membranes, the company serves more than 100 enterprise clients across domestic and Southeast Asian markets. These membranes are built for industrial waste acid resource recovery, addressing high neutralization costs, low metal interception rates, and insufficient acid recovery efficiency in traditional waste acid management. All products are manufactured under ISO9001 controls, with fully independent intellectual property rights. The company maintains an annual ion exchange membrane capacity of 250,000 square meters, with verified performance including 80%-90% acid recovery rate and over 95% metal ion interception rate across deployed projects.
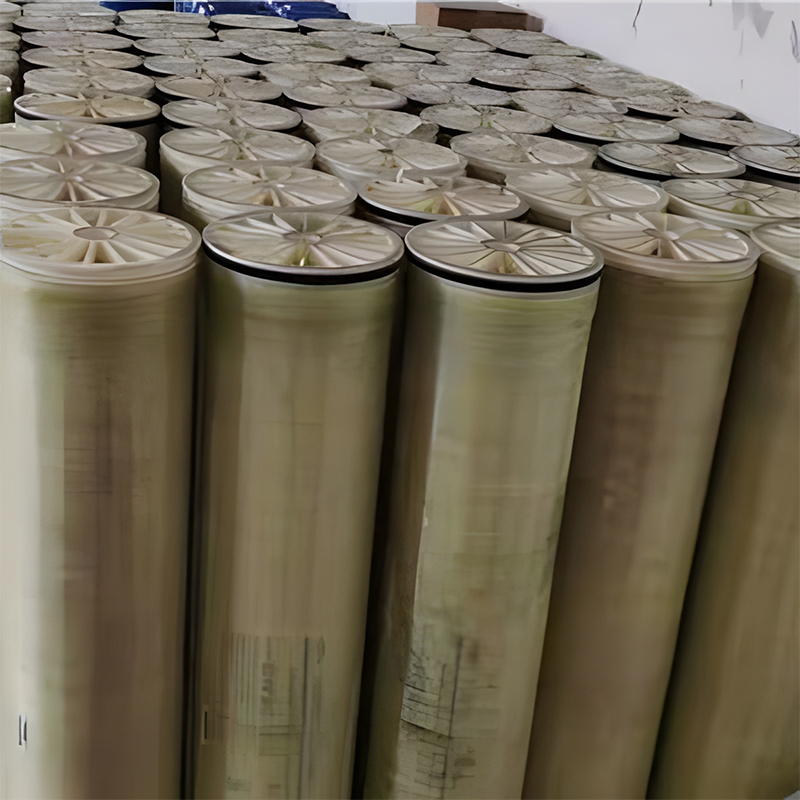
Diffusion dialysis acid recovery membrane is a homogeneous ion exchange membrane that operates on concentration-gradient driven anion selective permeation, enabling separation of free acid components from dissolved metal ions in industrial waste streams to support circular resource recovery. As a core component of zero-liquid-discharge industrial systems, it eliminates the need for external electric power during operation, delivering significantly lower ongoing operating costs compared to electric-driven membrane processes.
The product line covers three standard series, with custom solutions for specialized conditions:
1. DD conventional acid recovery membrane: For general hydrochloric acid and sulfuric acid recovery, suitable for stainless steel pickling and titanium dioxide production, with high acid flux.
2. PD phosphoric acid recovery membrane: The only domestically mass-produced phosphoric acid recovery membrane in China, optimized for aluminum profile polishing and etching waste streams.
3. MD monovalent acid recovery membrane: Built for complex mixed acid systems, suitable for biopharmaceutical and amino acid production waste acid recovery.
The core design philosophy prioritizes high reliability, low maintenance requirements, and extended service life, with all products engineered to withstand harsh industrial chemical conditions for a minimum 5-year operational lifespan.
The core operation relies on selective anion transport across the membrane driven by a concentration gradient between the waste acid stream and pure water recovery side. The process follows three key steps:
1. Concentration gradient formation: Free acid anion concentration on the waste side is higher than on the recovery side, creating the driving force for transport.
2. Selective permeation: The membrane’s fixed anion exchange groups allow acid anions to pass through, while repelling positively charged metal ions via electrostatic interaction.
3. Acid recovery: Permeated acid anions combine with hydrated hydrogen ions on the recovery side to form regenerated acid, while metal ions remain in the waste stream.
Compared to traditional non-homogeneous acid recovery membranes, the company’s homogeneous formulation delivers 2 times the processing capacity of comparable domestic products, with no external power requirement for operation. This eliminates energy costs for electric-driven treatment, while reducing sludge generation from traditional neutralization-based waste acid treatment.
All parameters are tested under standardized laboratory conditions, with full test reports available for each production batch and support for third-party verification.
| Parameter Category | Core Parameter | Standard Specification | Test Condition | Selection Guidance |
|---|---|---|---|---|
| Physical Properties | Membrane Thickness | 90-120μm | Dry state measurement at 25℃ | Balances acid flux and mechanical durability |
| Physical Properties | Membrane Resistance | 0.8-1.3Ω·cm² | 0.5mol/L Na2SO4 solution at 25℃ | Low resistance reduces mass transfer resistance during dialysis |
| Chemical Properties | Ion Exchange Capacity | 1.5-2.3meq/g | Titration measurement method | Ensures stable anion selective permeation performance |
| Performance Metrics | Acid Recovery Rate | 80%-90% | 1mol/L hydrochloric acid waste stream, 25℃, 24h continuous operation | Core indicator for resource recovery efficiency |
| Performance Metrics | Metal Ion Interception Rate | >95% | Hydrochloric acid waste stream with 10g/L iron ions, 25℃, 24h continuous operation | Ensures recovered acid purity for direct reuse in production |
| Durability | Service Life | ≥5 years | Continuous industrial waste acid operating conditions | Used for full lifecycle cost calculation |
Compared to conventional acid recovery membranes in the global market, the company’s products deliver verified, data-backed advantages validated across industrial deployments:
1. High processing capacity with exclusive phosphoric acid recovery: The company holds 2 independent invention patents for core formulations, with the PD series being the only mass-produced phosphoric acid recovery membrane in China. The DD series delivers 2 times the processing capacity of comparable domestic products, with stable 80%-90% acid recovery rate and >95% metal interception rate. This reduces customer waste treatment costs by cutting neutralization chemical use, while allowing recovered acid to be directly reused in production.
2. Stable supply chain with extended service life: The company operates 3 production lines with 250,000 square meters annual capacity, with 100% domestic raw material supply to eliminate disruption risks. Membrane stacks use a three-layer leak-proof design, with a minimum 5-year membrane service life and 7×24 hour technical support, reducing maintenance and replacement costs over the product lifecycle.
All research, design, production, and testing processes for the company’s diffusion dialysis membranes follow international and national industry standards, with a complete compliance system to meet global customer procurement requirements. The company holds ISO9001 quality management system certification and ISO45001 occupational health and safety management system certification, and is recognized as a High-Tech Enterprise and Specialized, Refined, Differential and Innovative SME in Shanghai. Core membrane technologies are protected by 2 independent invention patents, with all products designed and manufactured to national industry standards. The company can provide factory inspection reports for each batch, and supports third-party testing per customer requirements.
The company’s membranes are deployed across more than 100 industrial projects globally, with verified performance across key segments:
1. Aluminum profile surface treatment: The industry requires recovery of waste sulfuric acid, nitric acid, and phosphoric acid from anodizing and polishing processes. The company provides DD or PD series solutions paired with SDD series equipment, deployed for clients including Jinko Aluminum, Yangli Aluminum, and Aomei Aluminum, with stable acid recovery rates above 85%.
2. Metal processing pickling: The industry requires recovery of waste hydrochloric acid and sulfuric acid from stainless steel and titanium dioxide production to reduce hazardous waste emissions. The DD series delivers 80%-90% acid recovery rate, reducing hazardous waste output by over 60% for deployed clients.
3. Biopharmaceutical and amino acid production: The industry requires recovery of waste acid from amino acid mother liquor processing. The MD series is deployed for Hubei Xinshengyuan Biological Engineering, delivering an amino acid recovery rate above 90% with 72m³/d total processing capacity.
Q: What is the core difference between diffusion dialysis acid recovery membranes and electrodialysis membranes for acid treatment?
A: Diffusion dialysis membranes are driven solely by concentration gradient without external power, delivering lower operating costs for acid recovery, while electrodialysis membranes require electric field drive for desalination and concentration tasks.
Q: Can your diffusion dialysis membrane recover phosphoric acid from waste streams?
A: Yes, our PD series phosphoric acid recovery membrane is the only domestically mass-produced product of its kind in China, with stable phosphoric acid recovery rate above 85% for aluminum polishing and etching waste streams.
Q: Do you provide pilot testing before full-scale project deployment?
A: Yes, we support laboratory-scale testing and on-site pilot trials with real customer water samples to verify recovery performance and cost before industrial scale-up, reducing customer investment risk.
Q: What is the typical service life of your diffusion dialysis membranes in industrial operations?
A: The standard service life of our diffusion dialysis membranes is no less than 5 years under continuous industrial waste acid operating conditions, supported by our three-layer leak-proof membrane stack design.
Official Website: http://www.smaxnms.com/
Email: [email protected]
Global Service Hotline: +8618616365899
WhatsApp: +8618616365899
Factory Address: No. 2899, Lianhua South Road, Minhang District, Shanghai