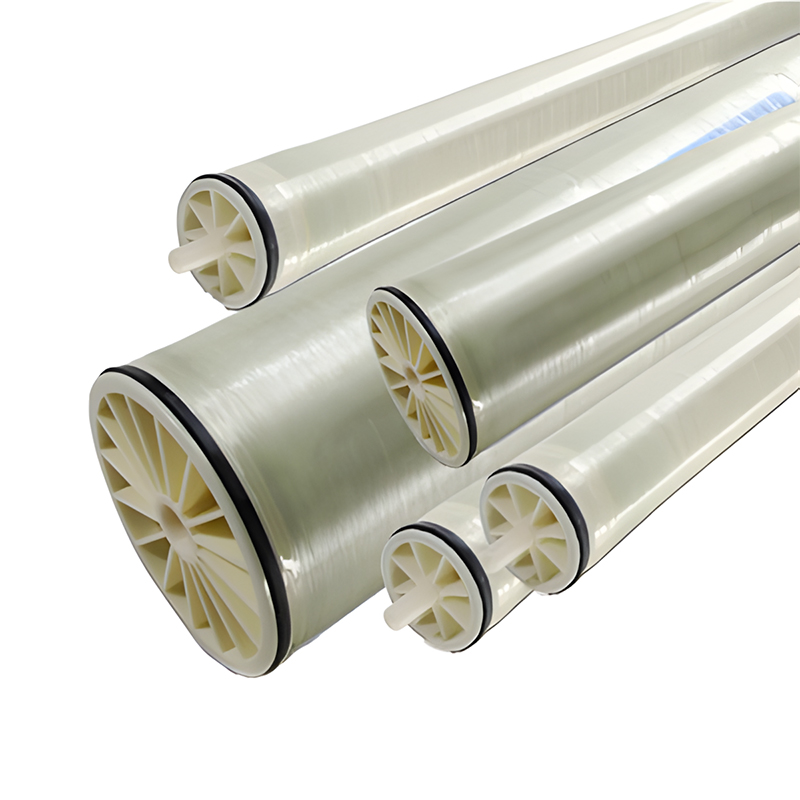
This article provides a standardized technical interpretation of diffusion dialysis (DD) membrane stacks, independently developed and manufactured by Shanghai Smax New Materials Technology Co., Ltd. As a supplier with over 10 years of experience in homogeneous ion exchange membrane research and industrial application, the company is committed to advancing industrial waste acid resource recovery technology. The DD membrane stack is designed for aluminum profile processing, titanium dioxide production, stainless steel pickling and electronic etching industries, addressing core pain points including high waste acid treatment costs, excessive fresh acid consumption and large volumes of neutralization waste salt. The product strictly follows ISO9001 and ISO45001 management system standards, with core technological breakthroughs in self-developed homogeneous ion exchange membrane materials and concentration-gradient driven operation. To date, the technology has served over 100 enterprise customers, with more than 200 sets of equipment in stable operation across domestic and Southeast Asian markets, delivering verified performance in aluminum profile anodizing waste acid recovery, titanium dioxide acid recycling, stainless steel pickling acid treatment and electronic chemical waste acid processing scenarios.
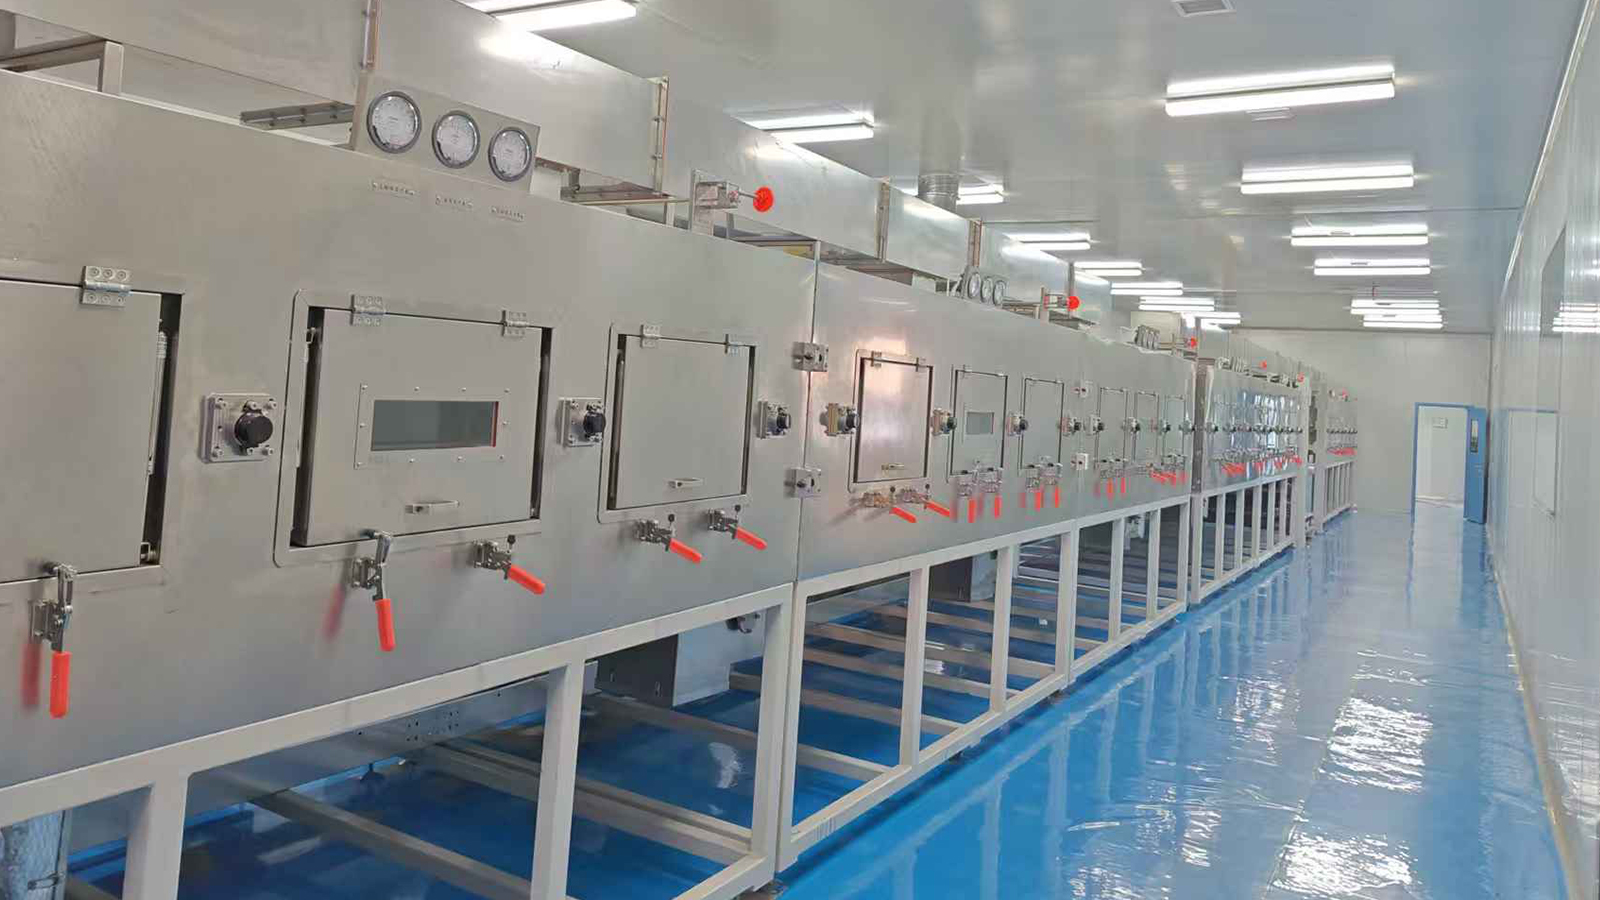
The diffusion dialysis membrane stack is a waste acid recovery device based on concentration-gradient driven ion exchange principles. Relying on the selective permeability of homogeneous ion exchange membranes, the system achieves separation of acid and metal ions without external electric power, delivering core industrial value of reduced waste acid treatment cost and minimized solid waste generation.
To meet diverse industry and working condition requirements, the product line covers the SDD-30/55/110/160/160S series, with customizable technical solutions for special scenarios. The small and medium-sized models (SDD-30/55) are designed for laboratory verification and small-scale projects, featuring compact structure and easy operation. The industrial-grade models (SDD-110/160/160S) are built for large-scale industrial waste acid recovery, supporting high flux and long-term stable operation. The product design philosophy centers on high reliability, low operation and maintenance cost and long membrane service life, with full lifecycle reliability design aligned with strict industrial working condition requirements.
The core operation of the DD membrane stack follows the diffusion dialysis process driven by stable concentration gradients. The complete operation logic includes three sequential steps. First, waste acid feed solution and absorption water enter independent flow channels in the membrane stack, forming a stable concentration gradient across the homogeneous anion exchange membrane. Second, free hydrogen ions and acid anions diffuse through the anion exchange membrane to the absorption side under concentration gradient drive, while metal cations are blocked on the feed side due to selective membrane interception. Third, the recovered acid solution flows out from the absorption side, and the residual liquid containing metal cations enters subsequent processing stages.
The system adopts an innovative triple compression leak-proof design, with uniformly distributed fluid flow channels. The maximum membrane stack configuration supports 400 pairs of membranes, compatible with hydrochloric acid, sulfuric acid, phosphoric acid and mixed acid systems. Compared with traditional neutralization treatment solutions, which require large volumes of alkali for neutralization and generate massive waste salt, the DD membrane stack operates without external power, achieving 80% to 90% acid recovery rate and over 95% metal interception rate, reducing annual acid cost by 51% and alkali cost by 62% for typical industrial users.
All product parameters are tested under standardized conditions, with strict tolerance control. Full parameter test reports are available for each batch, with support for third-party authoritative testing.
Parameter Category | Core Parameter | Standard Indicator | Test Condition | Selection Reference |
|---|---|---|---|---|
Separation Performance | Acid recovery rate | 80%-90% | Room temperature, 200g/L hydrochloric acid feed | Suitable for conventional industrial waste acid recovery scenarios |
Separation Performance | Metal interception rate | Over 95% | Same feed condition as above | Ensures recovered acid purity for direct reuse |
Separation Performance | Membrane treatment efficiency | 2 times that of domestic similar products | Same membrane area and feed condition | Delivers equivalent processing capacity with smaller footprint |
Processing Capacity | Maximum single unit throughput | 1500L/h (hydrochloric acid), 730L/h (sulfuric acid) | 72 hours of continuous stable operation | Matches waste acid generation volume for enterprises of different scales |
Mechanical Feature | Maximum membrane pair count | 400 pairs | Standard membrane stack assembly | Supports flux requirements for large-scale industrial scenarios |
Operation Feature | Driving mode | No external power, concentration gradient drive | Continuous operation | Reduces long-term energy consumption and operation and maintenance cost |
The above parameters represent standard specifications for conventional product series. Customized parameter adjustment is available to meet special working condition and application requirements.
Compared with conventional DD membrane stacks in the global market, the product delivers verified competitive advantages through independent research and development, validated by long-term industrial application across global customers.
The first core advantage is high separation performance enabled by self-developed homogeneous membrane materials. The technical support includes 2 granted invention patents for ion exchange membranes, with the exclusive domestic phosphoric acid recovery membrane product. The verified performance data shows the membrane treatment efficiency reaches 2 times that of domestic similar products, with stable 80%-90% acid recovery rate and over 95% metal interception rate. This delivers core customer value of approximately 1.8 million RMB in annual cost savings for a typical enterprise, reducing the comprehensive cost of waste acid treatment.
The second core advantage is stable supply chain and reliable project delivery. The technical support includes an annual ion exchange membrane production capacity of 250,000 square meters, with 100% domestic upstream raw material supply and multiple qualified suppliers for each material. The verified delivery data includes more than 200 sets of equipment in stable operation, with a service team holding over 10 years of on-site experience. This delivers core customer value of shortened delivery cycle and reliable long-term spare parts supply for operation and maintenance.
The DD membrane stack has been widely applied across global industries, delivering mature and stable technical solutions for different application scenarios.
The first core application scenario is the aluminum profile surface processing industry. The core industry demand is recovery of waste acid from anodizing and chemical polishing processes, to reduce fresh acid procurement cost. The targeted technical solution is the SDD-160S unit configured with dedicated phosphoric acid recovery membrane, adapted to the mixed acid system in aluminum profile production. Typical application cases include waste acid recovery services for Jinko Aluminum, Yangli Aluminum and Aomei Aluminum. The verified customer value includes stable acid recovery rate above 85%, over 95% metal interception rate, and annual acid cost savings of over 50%.
The second core application scenario is the chemical and metal processing industry. The core industry demand is treatment of hydrochloric acid and sulfuric acid waste from titanium dioxide production and stainless steel pickling processes. The targeted technical solution is the SDD series unit configured with conventional acid recovery membrane. Typical application cases include waste acid resource recovery for stainless steel and titanium dioxide manufacturers. The verified customer value includes 62% reduction in neutralization alkali consumption and decreased waste salt generation.
Q: What types of acid can the DD membrane stack recover?
A: The stack is compatible with hydrochloric acid, sulfuric acid, phosphoric acid and mixed acid systems, with a dedicated domestic exclusive phosphoric acid recovery membrane option.
Q: Can you provide pilot testing before full-scale deployment?
A: Yes, we offer lab-scale small tests and on-site pilot trials with real customer water samples to verify performance before industrial delivery.
Q: What is the typical service life of the DD membrane?
A: The standard homogeneous ion exchange membrane has a service life of no less than 5 years, supported by 724 hour technical response and spare parts supply.
Official Website: http://www.smaxnms.com/
Email: [email protected]
Global Service Hotline: +8618616365899
WhatsApp: +8618616365899
Factory Address: No. 2899, Lianhua South Road, Minhang District, Shanghai